1. What Is Pipe Pickling?
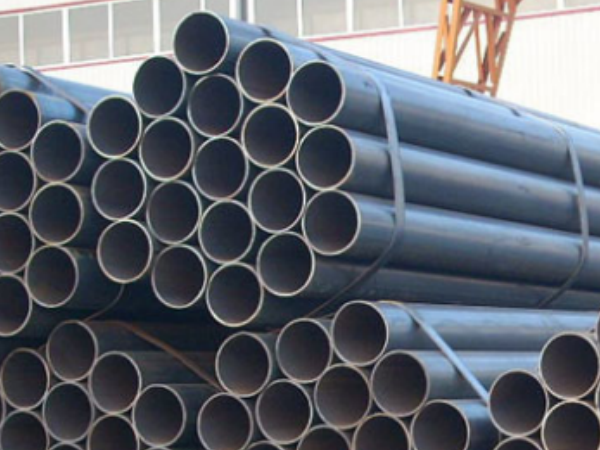
Pipe pickling is a chemical surface treatment process that uses an acid solution to remove rust, mill scale, and other surface impurities from the inner and outer surfaces of steel pipes. For seamless steel pipes, pickling is used to clean the metal surface after manufacturing or heat treatment and prepare it for subsequent processes such as coating, drawing, or passivation.
The acid system and process conditions depend on the pipe material, surface condition, and production requirements. After pickling, the pipes are rinsed and may undergo neutralization, passivation, drying, or another protective treatment when specified.
2. Why Are Seamless Steel Pipes Pickled?
Seamless steel pipes are pickled to remove surface contaminants such as rust, mill scale, iron oxides, oil, and grease that remain after manufacturing or heat treatment. Acid pickling removes these deposits and exposes a cleaner metallic surface, resulting in a smoother and more uniform surface condition.
A clean surface provides better conditions for subsequent processes such as coating, phosphating, galvanizing, drawing, or passivation when specified. Removing contaminants before these treatments can also improve coating or protective-film adhesion and reduce surface-related corrosion risks.
After pickling, the pipes are thoroughly rinsed and may receive a specified protective treatment before drying. Drying and temporary protection help prevent immediate re-rusting while the pipe is waiting for the next manufacturing or surface-treatment step.
3. Seamless Steel Pipe Pickling Process
The pickling process generally includes surface cleaning, acid treatment, rinsing, and drying. Depending on the pipe material and subsequent requirements, neutralization or passivation may also be included.
3.1 Pre-Cleaning and Degreasing
The pipe surface is first cleaned to remove oil, grease, dust, and other contaminants that could interfere with the acid treatment. Alkaline cleaning solutions or suitable degreasers may be used, followed by rinsing when required.
3.2 Acid Pickling
The cleaned pipes are immersed in an acid solution or treated by acid spraying. The acid dissolves rust, mill scale, iron oxides, and other oxide deposits from the pipe surface.
Common pickling systems include hydrochloric or sulfuric acid for suitable carbon steel applications. Other acid systems may be selected for stainless steel or specific alloy materials. Acid concentration, temperature, and treatment time are controlled according to the pipe material, surface condition, and process requirements.
3.3 Rinsing and Neutralization
After acid treatment, the pipes are thoroughly rinsed to remove residual acid and dissolved contaminants. Where required, a neutralization step or alkaline rinse is used before the next treatment.
3.4 Passivation When Specified
For stainless steel pipes, passivation may follow pickling when required by the material, specification, or application. This treatment promotes a more stable passive surface and is distinct from the acid pickling step itself.
3.5 Drying and Temporary Protection
After the final rinse or passivation, the pipes are dried to remove residual moisture. A suitable protective treatment may then be applied where necessary to help prevent immediate re-rusting during storage or before the next manufacturing or surface-treatment operation.
4. Which Seamless Steel Pipes Require Pickling?
(1) Stainless steel seamless pipes are commonly pickled when heat treatment or manufacturing leaves oxide scale or other surface contamination.
(2) Carbon steel seamless pipes may also require pickling when significant rust, mill scale, oil, or other contaminants remain on the surface, particularly before coating, galvanizing, phosphating, or drawing. The treatment conditions should be selected according to the steel grade and required surface condition.
(3) Precision seamless pipe pickling requires controlled acid concentration, temperature, and treatment time to remove mill scale while limiting excessive metal loss, surface attack, and pitting.
5. Pickling, Passivation and Subsequent Surface Treatment
Pickling removes mill scale and surface oxides, while passivation is a separate treatment, primarily used for stainless steel, that helps establish or restore its passive surface. After pickling, tubes are thoroughly rinsed and may undergo neutralization, passivation, coating, phosphating, or temporary rust protection according to the material and subsequent requirements. Drying and temporary protection help prevent flash rusting before further processing or storage.
6. FAQs
Q1: What is steel pipe pickling?
A: Chemical pickling is a surface cleaning process that uses an engineered acid solution to dissolve mill scale, rust, iron oxides, and heat-treatment scale from the inner and outer pipe surfaces.
Q2: Do all seamless steel pipes require pickling?
A: No. Pickling requirements depend on the pipe material, surface condition, manufacturing process, and downstream requirements. Stainless steel and precision cold-drawn tubes are commonly pickled when heat treatment leaves oxide scale or when a clean surface is required for subsequent processing. Carbon steel pipes may be pickled before coating, galvanizing, or other specified surface treatments.
Q3: What acids are used for pipe pickling?
A: Carbon Steel: Hydrochloric Acid (HCl) or Sulfuric Acid (H₂SO₄) are commonly used. Stainless Steel / High-Alloy: Pickling systems may use nitric acid (HNO₃), hydrofluoric acid (HF), or other formulated acid mixtures, depending on the alloy and oxide scale.
Q4: What is the difference between pickling and passivation?
A: Pickling is a cleaning process that removes scale, rust, and other surface impurities. Passivation is a separate treatment, primarily used for stainless steel, that helps establish or restore the passive surface responsible for its corrosion resistance.
Q5: Does pickling affect tight dimensional tolerances?
A: Controlled pickling removes surface scale without intentionally changing the specified pipe dimensions. For precision cold-drawn seamless tubes, acid concentration, temperature, treatment time, and inhibitor control are important to limit excessive metal removal, surface attack, or pitting.
Q6: What happens to seamless pipes immediately after pickling?
A: After pickling, pipes are thoroughly rinsed to remove residual acid and may undergo neutralization or passivation when specified. They are then dried, and a suitable temporary protective treatment may be applied to help prevent flash rusting before further processing or storage.
Related Articles
Cold Drawn Seamless Steel Pipe
EN 10305-1 Seamless Precision Tube
Surface Crack Analysis of Stainless Steel Seamless Pipe

 Eastern Steel Manufacturing Co.,Ltd not only improve product production and sales services, but also provide additional value-added services. As long as you need, we can complete your specific needs together.